Ready to eat (RTE) meat products have short shelf lives unless special precautions are taken to maintain and extend their shelf life. They are subject to spoilage by various bacteria that cause organoleptic and eating quality changes that make them unacceptable to consumers.
They are also subject to some pathogenic bacteria that can cause food borne illnesses.
The most prominent is Listeria monocytogenes. This particular organism is found commonly in the environment, but it is eliminated in food processing plants by proper cleaning and sanitation.
Various interventions have been researched over the past 25 years that can reduce the risk of the presence of Listeria in RTE meat products.
The most common methods include the use of various anti-Listeria ingredients, higher levels of sanitation and high-pressure processing (HPP). During HPP, the food product, encased in its package, is subjected to ultra-high pressure for a specific period of time.
The high pressure is sufficient to inactivate various bacteria, including Listeria, without compromising the nutritional value and quality of the food product. The HPP process has been used for many years by several large meat processors in the USA and is a proven non-thermal technology that does not change the ingredient profile of the food product.
Typically, packages of the product are placed into the HPP vessel filled with water where the pressure is increased to about 87,000 psi for around three minutes, then the pressure is released. The whole process including the time to come to pressure, hold and decompress takes approximately 10 minutes per batch.
High Pressure Processing (HPP) is Good, But Has Practical Limitations
There are many aspects of HPP that offer unique benefits through its use. However, its impact of sustainability over ingredient processing could be significant.
Are There Other Options to HPP?
Fortunately, Listeria is sensitive to weak organic acids; consequently, ingredient interventions containing such compounds/chemicals have been found to inhibit the growth of Listeria throughout the whole shelf life of the product, even after package opening.
These weak organic acids include vinegar (acetic acid), potassium and sodium lactate, sodium diacetate and other versions thereof.
Many of these ingredients are produced from various fermentations and result with the inclusion of some anti-Listeria peptides as well. An ingredient solution may also provide a more sustainable solution in the production of RTE meat products compared to HPP for several reasons:
- More sustainable packaging is possible when it does not need to withstand ultra-high pressures.
- Providing some protection post-opening (secondary shelf life) has the potential to reduce food waste.
- More streamlined processing lines and reduced potential for bottlenecks and extra transportation.
- Improved supply chain flexibility for decarbonization.
A unique blend of organic acids and peptides can improve product quality through clean label inhibition of pathogens and spoilage in RTE poultry products. This product can be used in uncured (no added sodium nitrite) and can work in high moisture-containing poultry products.
It results in a more natural colour and flavour and is efficacious against Listeria, Clostridium perfringens and Clostridium botulinum as well as some spoilage organisms. The product is labelled as “buffered vinegar and cultured dextrose” which falls into the more “clean label” category.
It has a less expensive cost-in-use than HPP. Studies at the Food Research Institute (University of Wisconsin) have shown no growth in Listeria for 14 weeks (1) when used in a low sodium turkey product (76% moisture, pH 6.2, 1.55% salt) when used at a rate of 2.0% (Fig. 1).
In addition to Listeria, this combination was successfully able to control resistant lactic acid bacteria in fresh poultry (2) and beef systems (3).
Figure 1: Listeria monocytogenes control with Buffered Vinegar and Cultured Dextrose
HPP’s Impact on Food Waste
In a case study where HPP-processed meat waste volumes were measured in foodservice and retail deli counter environments. The main sources were from damaged packaging and products that were not consumed/sold in the short shelf-life after opening.
The value captured was significant enough to warrant exploring the waste reduction from the secondary shelf-life extension that would occur through the potential replacement of the process with an ingredient-based solution.
Add this to the difference in environmental resources required for the ingredient-based approach versus the energy-intensive process and the impact of the switch became compelling4.
The Kerry Food Waste Estimator was used to give an indication of the volumes of waste that would be reduced downstream through the extra days after opening delivered by the switch.
Conclusions
The old saying that one size does not fit all applies to the different anti-Listeria interventions available to meat processors in the production of RTE meat products. Listeria monocytogenes represents a real threat to the safety of consumers.
This is because of increased monitoring, sanitation and the use of effective antimicrobial interventions. Meat processors have the options of various proven interventions including HPP and various ingredients.
The choice of which to use depends upon the company’s business goals and food safety philosophy. So, one shoe does not fit all sizes.
What are Enzymes?
Enzymes are proteins produced by all living organisms. They are biological catalysts which conduct all biochemical reactions.
This is a natural part of physiological processes essential for growth and allow life. When your body wants to transform food such as starch in bread or pasta into energy enzymes are used to convert the starch to simple sugars which can be used by your cells.
Enzymes are efficient, and specific performing typically only one defined reaction over and over again. The fact that they come from nature means that they act at specific pH and temperature conditions/ranges, which make them sustainable and biodegradable alternatives to chemical processing in the food industry.
Industrial enzymes can be extracted from plants or produced by microbial fermentation and purified.
Why are Enzymes in Food?
Enzymes have been used in food production for thousands of years. Our early ancestors discovered that cows stomach could turn milk into cheese.
Today, we use enzymes in food to manufacture of everything from bread, wine, beer, juice and dairy processing and much more besides.
In the bakery industry, different type of enzymes can be used as a natural way to keep bread softer for longer, enhance dough tolerance during processing or allow for reduction the egg content.
Enzymes also enable manufacturers to use local grains like cassava to make beer and make dairy products suitable for those with lactose intolerance.
Sustainability Benefits of Enzymes in Bakery
In the bakery industry, different type of enzymes are a natural way to optimize raw material performance despite varying/seasonal quality, enhancing manufacturing efficiencies, softness, moistness, antistaling or desirably sensory properties of baked goods over extended shelf life, reducing additives and energy usage, food loss and food waste, with sustainability benefits.
A recent environmental footprint estimated calculation found that (www.epa.gov) just 1 loaf of bread releases 1.15kg of CO2 emissions and uses 194L of water, which is equivalent to the same CO2 emissions from fully charging 140 smart phones and 2 average daily showers.
Delving deeper into food waste, according to United nations environment programme up to 10% of GHG are linked to uneaten food, and 30% of all food produced in wasted, costing the global economy over $900 billion per year.
More especially the various type of bakery enzymes are offering different functionalities. Maltogenic amylase allows to keep bread softer for longer, to extend shelf life, by improving product sensory characteristics and appearance over longer shelf life, prolonging the onset of staling characteristics and reducing likelihood of food being wasted at home.
Xylanases are known to improve dough tolerance during processing. Asparaginase, to make baked good healthier by reducing the acrylamide content.
Some phospholipases allow to successfully reduces egg content by up in fine bakery applications such as muffins, stirred cakes, whipped cakes, croissants, donuts and brioche, with no change in dough handling or crumb structure versus a full egg recipe, eggs being crucial to bakers because of their specific functional properties and unique contribution to finished product sensory attributes: texture, softness, crumb structure, taste, including “binding”, “aeration”, “emulsification” and “colour”.
How Can Enzymes be Used for Nutrition & Health?
Digestive Enzymes – Reducing Lactose Intolerance Symptoms with Lactase
Lactose, the sugar found in dairy products, can cause problems like bloating and other gastrointestinal discomforts in people with lactose intolerance.
Lactose intolerance affects a significant amount of people worldwide, especially in places where dairy farming is not common. The incidence of lactose intolerance can be as high as 75% of the population in these areas.
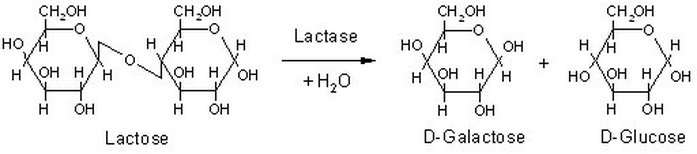
Enzymes can help lactose intolerant individuals enjoy dairy products with minimal side effects. Lactose is a sugar made of two smaller sugars: galactose and glucose (see figure below).
These sugars have a greater relative sweetness than lactose meaning that lactose free or low-lactose products that have been made with the lactase enzyme are sweeter in taste than those not treated with lactase.
In the food industry this can allow dairy products like yoghurt to be made with a reduced amount of added sugar but with the same taste profile.
Lactase is an enzyme that cleaves lactose into these two smaller sugars, neither of which cause the negative side effects of lactose in those with lactose intolerance. This is why you see the ingredient ‘lactase’ in lactose-free milks, for example.
Digestive Enzymes – Helping Infants Digest Formula
It is recommended by the world health organisation that infants be exclusively breastfed for the first six months of life so as to give the infant the greatest chance of achieving optimal growth, development and health, but for cases where this is not realistic or possible, infant formula is required.
Some infants have a hard time digesting certain types of formula, but enzymes can help in a few ways.
Comfort Protein – Infant Milk Formula (IMF)
Comfort infant formulas are made with partially hydrolysed milk proteins which are marketed as “easier to digest” infant formula made from cows milk.
These formulas can be produced using natural enzymes, called proteases, which target proteins and are derived from animal, plant or microbial sources.
Hydrolysis of milk proteins by proteases results in the formation of smaller peptides which are reported to be more readily digested than intact proteins.
In particular, parents of infants suffering from conditions such as colic, cite the use of comfort protein as reducing the severity of symptoms.
Hypoallergenic Formulas (IMF)
Most common IMFs use cow’s milk as a base, but a small percentage of infants are born with cow’s milk protein allergy (CMPA).
Formulas sold to address this condition can be divided into two types – those which are extensively hydrolysed (peptide-based) and those which are amino acid based.
Extensively hydrolysed proteins for this application are produced via enzymatic hydrolysis where the protease enzyme extensively breaks down the structure of the whey and/or casein protein to smaller peptides.
From the American Academy of Family Physicians: “Hypoallergenic formulas contain extensively hydrolyzed proteins that are less likely to stimulate antibody production. Infants with milk protein allergy fed hypoallergenic formula have slightly greater weight gain during the first year than infants fed standard formula. In addition, many infants show improvement in atopic symptoms. A few infants continue to have symptoms despite switching to hypoallergenic formula; nonallergenic amino acid–based formulas are effective for these rare cases.”
Enzymes for the Plant-Based Trend
The market for nutritional beverage is growing and cereal based beverages such as Horlicks, Bournvita, etc. have traditionally been very popular in certain markets.
The plant-based beverage market has continued to grow with milk-alternatives like soy or oat milk.
Enzymes are often used to help make these beverages more acceptable to consumers. For example, plant-based beverages like oat or rice milk can have poor emulsion stability, meaning products might separate out over their shelf life instead of remaining a consistent mixture.
Enzymes like amylase can help improve stability of the product. Much like lactase, amylase can also reduce the need for added sugar because the products of starch hydrolysis are sweeter than the starch itself.
If high viscosity is caused by high molecular weight (Mw) beta-glucan, as in the case of a beverage like oat milk, beta-glucanase can be used to make an easier to process, less viscous product.
However, since beta-glucan is the fiber associated with health benefits in oats, cleaving beta glucan with an enzyme would likely reduce the potential health benefit. If health benefits and fiber content are a focus, beta glucanase may not be the best solution.
Making Plant-Based Protein Hydrolysates Taste Better
With the rise in demand for plant-based proteins, there has been an increased demand for inexpensive plant-derived protein hydrolysates, owing to their significant potential in nutritional applications.
Hydrolysed plant protein (HPP) is most commonly produced via the enzymatic hydrolysis of a plant protein source such as soy, wheat, rice, sunflower, potato and alternative pulse proteins, and are used in a wide variety of food applications such as protein fortified bars and beverages.
Protease enzymes are most commonly used in the production of HPPs and under controlled conditions are used maximise protein yields from different plant sources and also to improve taste and sensory attributes.
From a commercial standpoint, plant proteins maintain unique taste attributes, and today’s HPP products are synonymous with bitter, unpleasant tastes often attributed to a high concentration of hydrophobic free amino-acids, smaller peptides and volatile compounds in the HPP mixture.
Enzymatic hydrolysis, both pre- and post-hydrolysis can help to significantly improve these undesirable sensory properties of HPPs.
This article was originally published on 15 September 2020. It was updated 19 June 2023 to reflect new information.